| Process Duty and Feed Characteristics | Confirm the slurry type, solids concentration, particle-size distribution, mineralogy, settling behavior, temperature, pH, and corrosive constituents. | Define the design case using normal, minimum, maximum, and upset feed conditions. Record feed solids by mass, slurry density, flow rate, particle-size distribution, and overflow clarity target. | Use representative laboratory settling tests, hydraulic calculations, and pilot-scale thickening tests rather than relying only on nominal feed-flow data. |
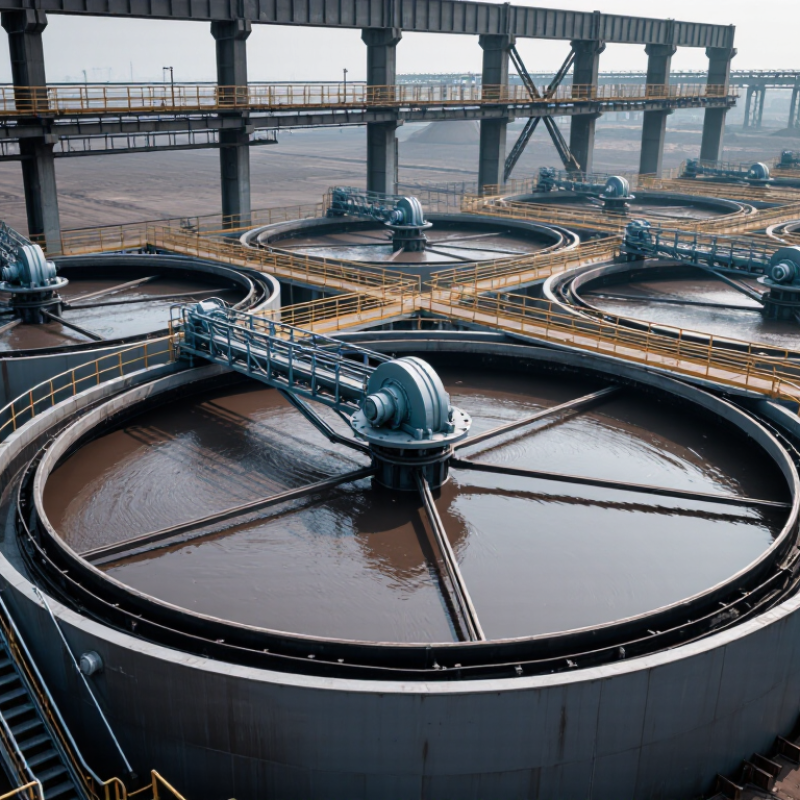
| Thickener Diameter and Capacity | Assess the required settling area, solids loading rate, hydraulic loading, and available installation space. | Size the unit from tested settling performance. Typical industrial units may range from several metres to more than 100 m in diameter, depending on duty and site requirements. Avoid selecting by tank volume alone. | Compare the supplier's design basis with measured test results and confirm capacity at the highest expected solids loading and flow rate. |
| Tank and Launder Materials | Evaluate structural steel, concrete, stainless steel, polymer linings, rubber linings, and corrosion-resistant coatings. | Carbon steel is commonly used for structural components when protected by a suitable coating. Stainless steel or lined surfaces may be justified for acidic, chloride-bearing, abrasive, or chemically aggressive service. | Review slurry chemistry, chloride level, abrasion potential, coating compatibility, design corrosion allowance, and inspection access. |
| Rake and Scraper Materials | Check the construction and wear resistance of rake arms, scraper blades, feedwell components, and mud-zone parts. | Common choices include coated carbon steel, stainless steel, abrasion-resistant steel, polyurethane, and replaceable rubber or polymer blades. The selection should reflect particle hardness, underflow density, and expected torque. | Request wear-life assumptions, replaceable-component drawings, and compatibility information for abrasive or corrosive slurry. |
| Feedwell Design | Evaluate feed dilution, energy dissipation, flocculant mixing, inlet velocity, and short-circuiting control. | A well-designed feedwell should distribute flow evenly, reduce turbulence, and allow flocs to form without excessive shear. Feedwell access should permit inspection and cleaning. | Review computational or physical flow studies where appropriate, and confirm expected overflow clarity and settling-zone behavior during testing. |
| Flocculant and Reagent System | Assess polymer preparation, dilution, aging time, dosing accuracy, injection location, and mixing intensity. | The optimum polymer dose is application-specific. The system should support controlled dilution and stable dosing over the normal operating range, with provisions for low-flow alarms and flushing. | Carry out jar tests or laboratory flocculation tests using actual process water and slurry. Verify polymer consumption per tonne of dry solids. |
| Drive and Torque Capacity | Evaluate the peripheral drive arrangement, gearbox, pinion and ring gear, lubrication, overload protection, and torque margin. | The drive should withstand normal operating torque, start-up loads, rake lifting events, uneven solids distribution, and short-duration upset conditions. The exact motor rating must be based on calculated torque, not tank diameter alone. | Review torque calculations, start-up analysis, overload set points, emergency-stop behavior, and the availability of a manual or auxiliary lifting arrangement. |
| Torque Measurement and Protection | Check whether torque is continuously measured and whether alarms, trips, and automatic corrective actions are provided. | Useful functions include high-torque warning, high-high torque trip, rake lifting, controlled restart, trend logging, and interlocks that prevent damage during overload conditions. | Request the cause-and-effect matrix and test each alarm, trip, reset, and fail-safe action during commissioning. |
| Underflow Density and Pumping | Assess underflow withdrawal points, discharge cone geometry, rake arrangement, pump type, and flow-control strategy. | The target underflow density must be established through test work. High-density underflow can increase yield stress and pumping power, so the pump and pipeline must be sized for the actual rheology. | Measure underflow density, flow rate, viscosity or yield stress where relevant, and pipeline pressure during a range of operating conditions. |
| Bed-Level Measurement | Evaluate bed-level instrumentation, measurement range, sensor fouling resistance, and redundancy. | Common technologies include sonar, ultrasonic, pressure-based, and radiometric measurement. The suitable technology depends on slurry density, gas bubbles, suspended solids, tank geometry, and maintenance restrictions. | Compare instrument readings with manual sampling or independent measurements during commissioning and seasonal process changes. |
| Density and Flow Instrumentation | Review online density meters, magnetic flow meters, pressure transmitters, pH instruments, and overflow turbidity monitoring. | Instruments should be selected for abrasive slurry service, adequate turndown, accessible isolation valves, and calibration without unnecessary process interruption. | Check wetted-material compatibility, accuracy specifications, calibration intervals, impulse-line design, and cleaning procedures. |
| Automatic Control Functions | Assess control of underflow flow, bed level, rake torque, dilution water, flocculant dose, and overflow quality. | A robust control strategy normally includes cascade or feedback control, high-torque protection, density-based underflow control, and alarms for abnormal bed level, flow, and instrument failure. | Review the control narrative, PLC or DCS interface, alarm priorities, trend screens, interlocks, and manual-operation fallback mode. |
| Remote Monitoring and Data Logging | Determine whether operating data can be monitored locally and remotely through the plant control system. | Useful data include torque, rake speed, bed level, underflow density, underflow flow, overflow turbidity, feed flow, polymer dose, motor current, and alarm history. | Confirm communication protocols, user access levels, time synchronization, historian retention, cybersecurity requirements, and loss-of-communication behavior. |
| Rake Speed Control | Check whether the rake speed is fixed or variable and whether it can be adjusted for changing solids loading. | Variable-speed control can help manage changing feed conditions, but rake speed must remain within the mechanical and process design limits to avoid excessive shear or unstable bed conditions. | Review the allowable speed range, control logic, gearbox limits, and operating procedure for high-solids or high-torque events. |
| Overflow Quality | Evaluate overflow weirs, launder levelness, scum removal, short-circuiting, and turbidity monitoring. | Evenly levelled overflow weirs and adequate launder capacity help reduce localized flow and solids carryover. The required turbidity or suspended-solids limit depends on the downstream process and water-reuse requirements. | Inspect weir alignment, perform hydraulic checks, and measure overflow suspended solids or turbidity under normal and peak conditions. |
| Foundation and Structural Loads | Confirm tank, bridge, walkway, drive, wind, seismic, hydrostatic, and sludge-load requirements. | Structural design should account for full-tank conditions, uneven sludge accumulation, maintenance loads, environmental forces, and accidental or abnormal operating conditions. | Review certified structural calculations, foundation loads, anchoring details, access platforms, guardrails, and applicable local design codes. |
| Lubrication and Sealing | Assess gearbox lubrication, ring-gear protection, bearing seals, grease points, and contamination control. | Lubrication points should be accessible from safe platforms. Automatic lubrication may reduce missed service intervals, while sealed or protected components can reduce contamination from water and solids. | Request lubrication schedules, lubricant specifications, inspection points, oil-analysis recommendations, and spare-seal requirements. |
| Inspection and Maintenance Access | Check access to the drive, gearbox, rake arms, feedwell, overflow launders, instruments, valves, and underflow equipment. | Walkways, platforms, ladders, lifting points, removable panels, and isolation valves should allow routine inspection without exposing personnel to unnecessary process hazards. | Review maintenance drawings, lifting plans, confined-space requirements, fall protection, and the estimated time for major component replacement. |
| Wear Parts and Spare Parts | Evaluate the availability, interchangeability, and replacement time for scraper blades, seals, bearings, pinions, sensors, valves, and liners. | Prefer modular, replaceable wear parts with clear part identification. Critical spares should be defined according to lead time, failure consequence, and site isolation capability. | Request a recommended spare-parts list, bill of materials, expected wear intervals, storage requirements, and documented replacement procedures. |
| Safety Systems | Review guarding, emergency stops, lockout points, overspeed protection, access control, and personnel protection around moving equipment. | The design should prevent access to rotating or moving parts during operation and provide safe isolation for inspection, cleaning, and maintenance. | Verify compliance with applicable machinery, electrical, structural, and workplace-safety requirements through a formal risk assessment. |
| Energy and Operating Cost | Compare motor power, rake-drive efficiency, pumping demand, polymer consumption, dilution-water use, and expected maintenance cost. | Total cost of ownership should include electrical energy, reagents, wear parts, lubrication, inspection labor, downtime, and disposal or treatment of process water. | Build a life-cycle cost model using measured or guaranteed operating ranges rather than motor nameplate power alone. |
| Commissioning and Performance Testing | Define acceptance criteria for capacity, underflow density, overflow quality, torque, control response, and equipment availability. | Performance testing should cover normal feed, design feed, start-up, shutdown, feed interruption, high-solids conditions, and instrument or communication failures. | Use a written commissioning plan with calibrated instruments, agreed sampling points, test duration, data-quality requirements, and corrective-action procedures. |
| Documentation and Training | Check the quality of operating manuals, maintenance instructions, drawings, control narratives, calibration records, and training materials. | Documentation should include process and instrumentation diagrams, spare-parts lists, torque settings, lubrication points, alarm descriptions, troubleshooting steps, and safe-work procedures. | Require operator and maintenance training before handover, together with final as-built drawings and an approved preventive-maintenance schedule. |