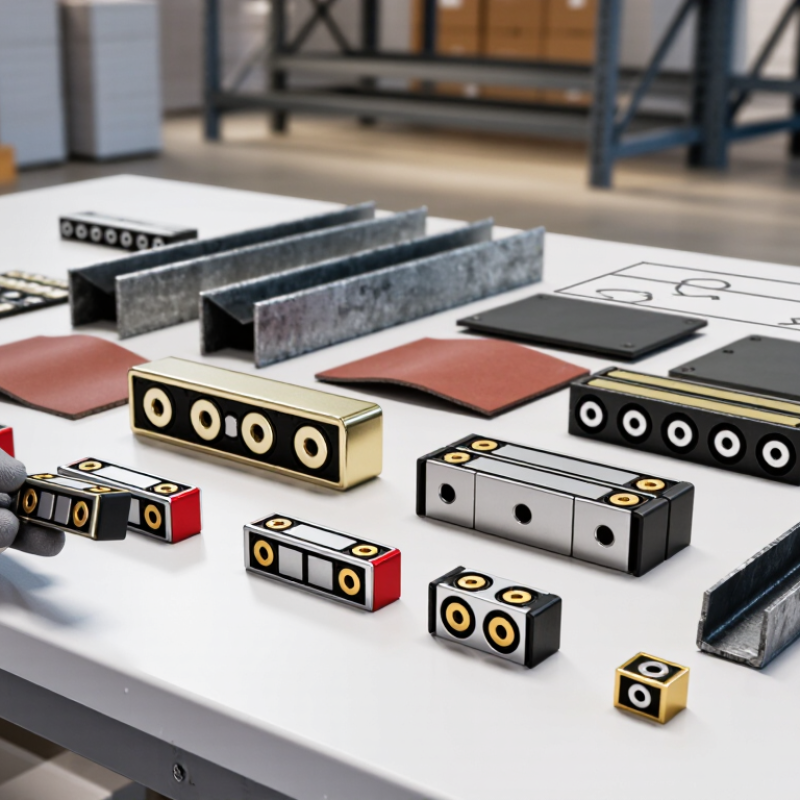
| 1 | Define the channel magnet design | Confirm the magnet material, steel channel dimensions, pole arrangement, coating, mounting method, and intended operating environment. | Record length, width, height, hole pattern, magnetic pole orientation, pull-force test method, and allowable dimensional tolerances in the drawing. | Approved 2D drawing, product specification, sample photographs, and a signed technical data sheet. | Freeze the specification before requesting quotations so suppliers quote comparable products. |
| 2 | Check the magnetic material standard | Determine whether the hard magnetic material used in the assembly is covered by the selected material specification. | IEC 60404-8-1 provides specifications for individual magnetically hard materials. It should be applied to the relevant permanent-magnet material, not treated as a blanket certification for the complete channel assembly. | Material grade declaration, lot-specific magnetic test report, and traceability from the material lot to the finished order. | Do not accept “IEC compliant” without identifying the applicable material grade and test basis. |
| 3 | Verify magnetic performance | Compare the required magnetic output with the supplier’s defined test conditions. | Specify the measured property, such as residual induction, coercive force, maximum energy product, surface flux density, or pull force. Pull force depends on air gap, steel thickness, contact area, and test fixture. | Calibration information for the gaussmeter or force gauge, test fixture drawing, sample results, and acceptance limits. | Use the same test method and fixture for supplier samples, pre-shipment inspection, and incoming quality control. |
| 4 | Evaluate corrosion and temperature resistance | Match the magnet coating and assembly materials to humidity, salt exposure, chemicals, and operating temperature. | Review coating type, exposed steel areas, adhesive temperature rating, and the magnet’s reversible and irreversible temperature limits. A coating choice alone does not guarantee corrosion resistance. | Coating specification, environmental test results where required, adhesive technical data, and visual inspection criteria. | Request an application-specific validation test when the product will be used outdoors, in wet areas, or near corrosive chemicals. |
| 5 | Confirm ISO 9001 status | Check whether the manufacturing site has a valid quality management system certificate. | ISO 9001 certification applies to a defined organization, site, and scope. It is evidence of a quality management system and is not, by itself, proof that every magnet meets the required performance. | Current certificate, certificate scope, issuing certification body, validity dates, and manufacturing-site address. | Verify the certificate through the certification body or an accredited certification directory where available. |
| 6 | Assess production capacity and supply continuity | Review normal lead time, monthly capacity, critical raw-material availability, tooling requirements, and backup arrangements. | Ask for a written production schedule covering sample approval, first production, routine production, inspection, and dispatch. Capacity figures should be linked to the specified product and quantity. | Capacity statement, production lead-time history, process flow, contingency plan, and defined escalation contact. | For repeat orders, approve a second source or maintain an agreed safety-stock plan for critical applications. |
| 7 | Clarify MOQ and price breaks | Identify the minimum order quantity for samples, standard production, custom tooling, and each configuration. | MOQ is commercially negotiated and is not fixed by IEC 60404-8-1 or ISO 9001. Request price tiers by quantity, setup charges, packaging charges, and any tooling or sampling fees. | Written quotation showing MOQ, unit price, lead time, payment terms, sample policy, and validity period. | Compare total landed cost at the expected annual volume rather than comparing unit price alone. |
| 8 | Select suitable Incoterms | Define which party controls transport, export clearance, insurance, import clearance, duties, and delivery to the named place. | Incoterms® 2020 should be stated with the named place or port. FCA is commonly used for containerized cargo; FOB is intended for sea or inland-waterway shipments when goods are loaded on board; DAP and DDP allocate different import responsibilities. | Quotation showing the exact rule, named place, shipment mode, cargo insurance responsibility, and customs-document responsibilities. | Do not compare EXW, FOB, CIF, DAP, and DDP prices as if they included the same logistics services. |
| 9 | Control inspection and acceptance | Agree on dimensional, visual, magnetic, coating, packaging, and quantity inspections before production begins. | Define sampling level or inspection quantity, critical dimensions, permissible defects, labeling requirements, and the procedure for handling nonconforming goods. | Inspection plan, approved golden sample, inspection report template, calibration records, and packaging checklist. | Use pre-shipment inspection for new suppliers or high-value orders, and retain batch records for traceability. |
| 10 | Review packaging, documentation, and import readiness | Ensure the shipment is protected from impact, magnetic interference, moisture, and handling damage. | Confirm carton dimensions, pallet requirements, product labels, packing list, commercial invoice, certificate of origin when needed, and any transport or customs documentation applicable to the shipment. | Packaging drawing, carton photos, final packing list, commercial invoice, quality report, and shipment tracking information. | Approve packaging samples for long-distance transport and verify document consistency before dispatch. |